ASP23 Powder Metallurgy HSS: Properties and Tooling Applications
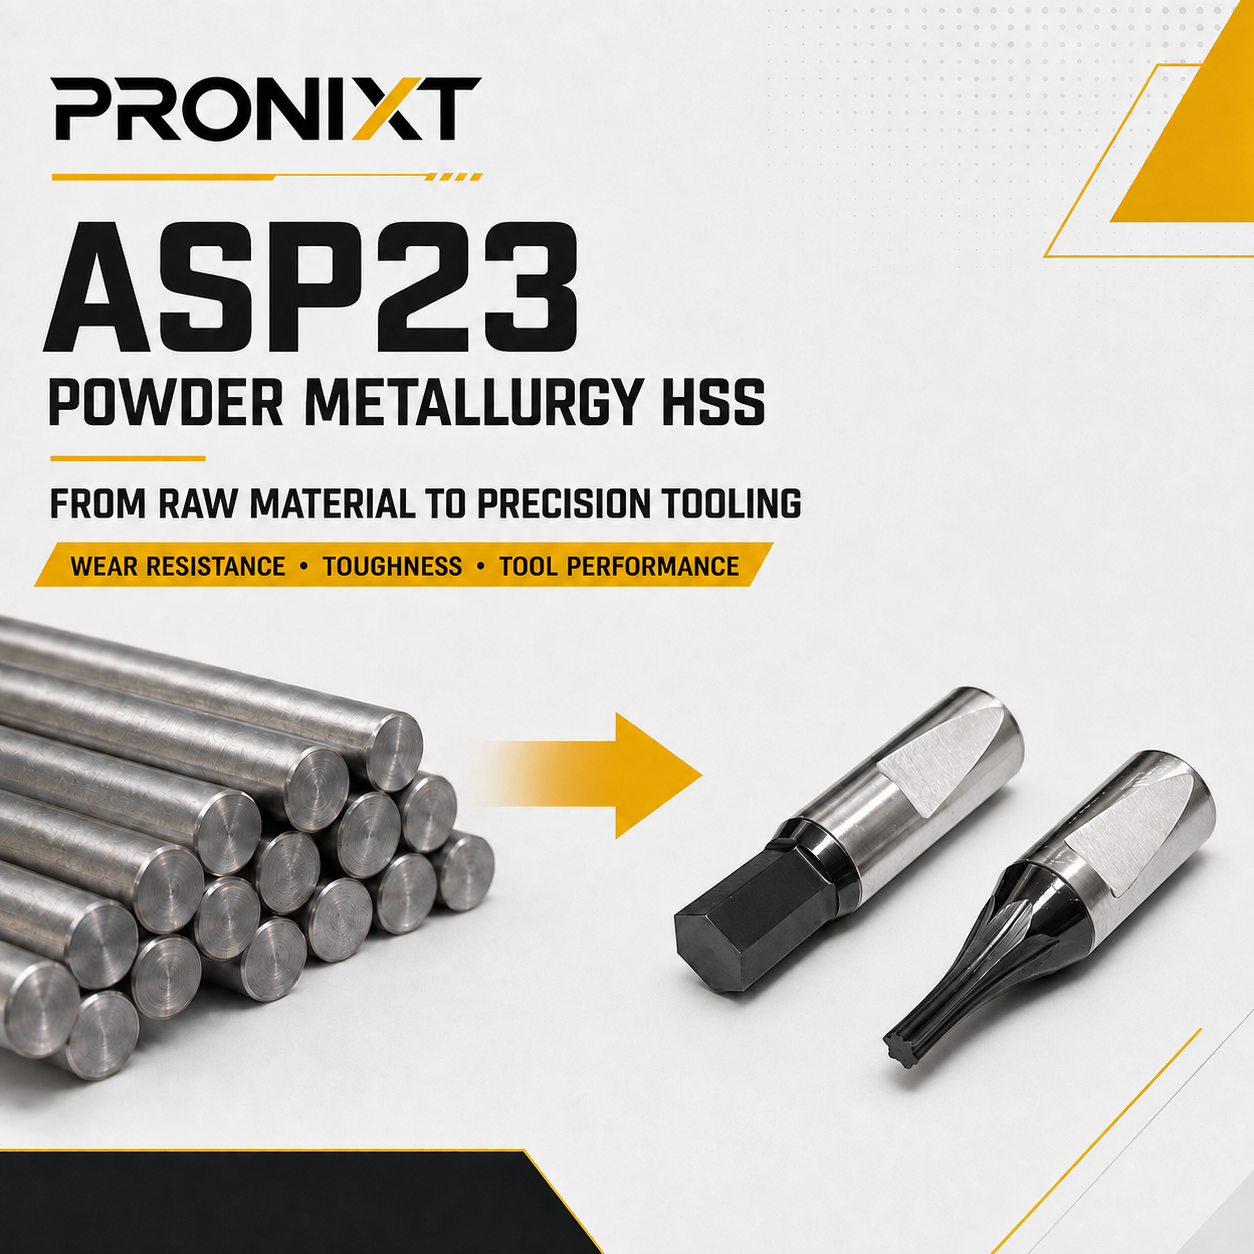
ASP23 combines wear resistance, compressive strength and toughness in a powder-metallurgy high-speed steel used for demanding precision cutting tools, including rotary broaches.
What Is ASP23 Powder Metallurgy HSS?
ASP 2023, commonly shortened in tooling discussions to ASP23, is a cobalt-free, highly alloyed powder- metallurgy high-speed steel. It is designed for high-performance cutting tools and demanding cold-work applications where the tool must resist wear without becoming unnecessarily brittle.
The grade corresponds to AISI M3:2 and is also associated with material designations 1.3395 and JIS SKH53. Its combination of carbon, chromium, molybdenum, tungsten and vanadium supports high hardness, abrasive-wear resistance and compressive strength after suitable heat treatment.
Why the Manufacturing Route Matters
Powder metallurgy is not simply another name for high-speed steel. It describes how the alloy is produced and consolidated to obtain a clean, uniform material suitable for precision toolmaking.
Alloy Preparation
The required alloying elements are melted in controlled proportions before powder production.
Powder Formation
The molten alloy is atomized into small particles, supporting a more uniform distribution of alloy constituents.
Consolidation
The powder is consolidated into dense material under controlled pressure and temperature.
Precision Toolmaking
The consolidated steel can then be machined, heat treated, ground and coated for the final application.
The Balance Required for Precision Tooling
Tool performance depends on more than maximum hardness. For small precision cutting forms, the substrate must combine wear resistance with sufficient toughness and dimensional control.
Wear Resistance
Helps the working profile resist gradual abrasive wear during repeated cutting contact.
Compressive Strength
Supports small cutting edges subjected to concentrated loads during forming and broaching operations.
Toughness
Provides resistance to premature edge chipping and cracking when the process is correctly prepared.
Dimensional Stability
Supports predictable heat treatment and precision grinding of the final tool geometry.
ASP23 Alloying Elements
The following nominal composition illustrates the alloy system used in ASP 2023 powder-metallurgy high-speed steel.
| Carbon C |
Chromium Cr |
Molybdenum Mo |
Tungsten W |
Vanadium V |
Cobalt Co |
|---|---|---|---|---|---|
| 1.28% | 4.0% | 5.0% | 6.4% | 3.1% | — |
Values shown are typical nominal figures. Published values may vary slightly by producer or product specification. Finished tool performance also depends on heat treatment, geometry, coating and machining conditions.
Why ASP23 Is Used for Precision Rotary Broaches
Rotary broaches combine a small precision profile with repeated cutting contact and concentrated loading. The tool material must support both form accuracy and edge reliability.
Small Cutting Profiles
Hexagonal, square and Torx-style forms contain narrow edges and corners that require a stable, wear-resistant tool substrate.
Concentrated Tool Load
The broach experiences compressive and cyclic loading as the cutting contact moves around the form.
Precision Grinding
Good grindability and dimensional stability help control the final profile, relief geometry and shank accuracy.
ASP23 Alone Does Not Determine Tool Life
Selecting a suitable steel is important, but reliable rotary broaching requires the complete tool and machining process to work together.
Material quality and cleanliness form the foundation for the finished cutting tool.
Hardening and tempering must balance wear resistance, strength and toughness for the intended tool geometry.
Profile dimensions, corner design, face geometry and relief directly affect cutting load and accuracy.
A suitable coating can support wear resistance and friction control, but cannot correct unsuitable tool geometry or heat treatment.
Correct hole preparation reduces unnecessary load and provides clearance for the required internal form.
Alignment, rigidity, lubrication, speed, feed and chip relief all influence process stability.
ASP23 Substrate and Tool Coatings
The coating is selected after considering the workpiece material, tool geometry and machining conditions. It works together with the ASP23 substrate rather than replacing it.
Provides the underlying balance of hardness, wear resistance, compressive strength and toughness.
Available for suitable applications where additional wear resistance and friction control are required.
The coating can be evaluated according to the part material, form dimensions and operating conditions.
ASP23 Powder Metallurgy HSS FAQ
Is ASP23 the same as ASP 2023?
Does ASP23 contain cobalt?
Why use powder-metallurgy steel for rotary broaches?
Is ASP23 always better than conventional HSS?
Does coating determine rotary-broach tool life?
Can PRONIXT manufacture custom ASP23 rotary broaches?
Need an ASP23 Rotary Broach?
Send us the required profile, dimensions, broaching depth, workpiece material, machine model and technical drawing for evaluation.