What Is Rotary Broaching? How Internal Hex, Square and Torx Forms Are Made
Rotary broaching is a precision machining process used to produce internal polygon forms in one continuous pass on CNC lathes, Swiss-type machines, screw machines and machining centers.
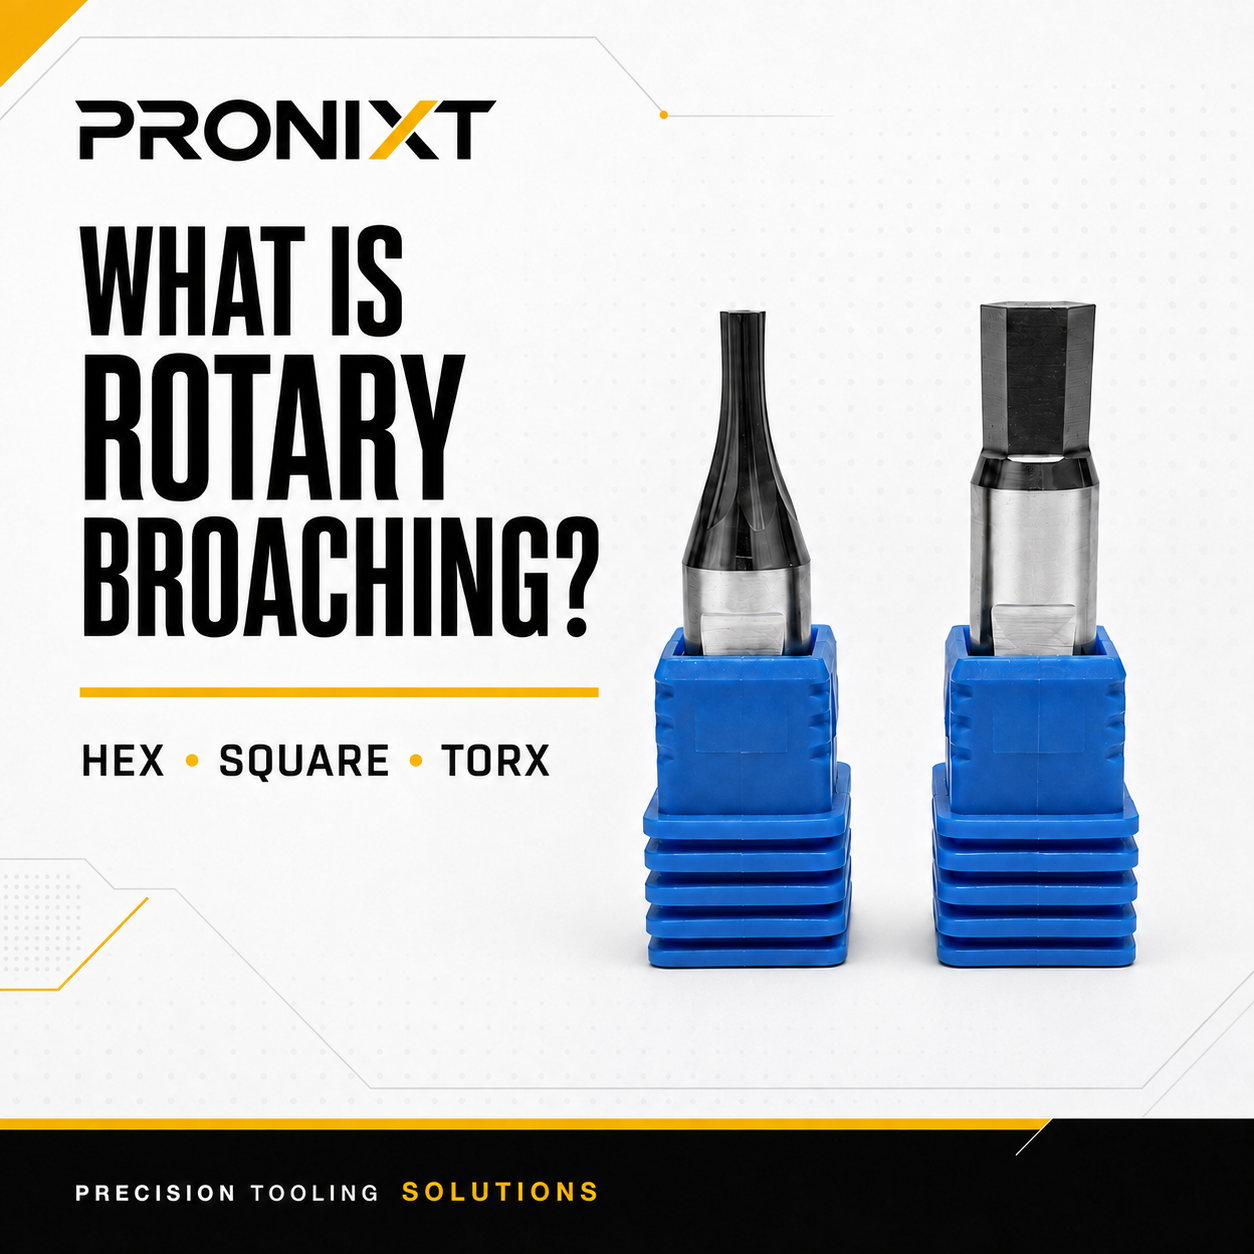
Producing a Complete Internal Form in One Pass
Rotary broaching, also known as wobble broaching, forms a polygon-shaped hole by feeding a specially ground broach axially into a prepared pilot hole. The broach is positioned at a slight angle relative to the workpiece axis.
As rotation continues, cutting pressure moves progressively from one cutting edge to the next. The complete profile is therefore not forced into the material at full depth at the same instant.
This progressive cutting action makes it possible to produce hexagonal, square, Torx-style and other internal forms directly on the primary CNC machine without a separate secondary broaching operation.
The Rotary Broaching Process
The process combines a prepared pilot hole, a suitable entry chamfer, the rotary broach holder and controlled axial feed.
Prepare the Pilot Hole
Drill or bore the starting hole to the calculated diameter required for the profile and workpiece material.
Add the Entry Chamfer
A suitable chamfer allows the cutting corners to enter the workpiece smoothly without excessive initial impact.
Feed the Broach
The holder positions the broach at a slight angle while the machine provides rotation and controlled axial feed.
Complete the Form
Cutting progresses around the profile until the specified depth and complete internal form are reached.
Why Rotary Broaching Uses a Slight Angular Offset
The angular relationship between the broach and the workpiece creates the controlled wobbling motion responsible for the rotary broaching process.
Slight Holder Angle
Rotary broach holders commonly use a small built-in angular offset. The exact design depends on the holder system and application.
Successive Edge Contact
Cutting pressure moves around the face of the broach instead of loading the entire polygon profile simultaneously.
Continuous Axial Feed
The tool advances along the workpiece axis until the required form depth is achieved, then retracts from the completed feature.
Correct Part Preparation Is Essential
Incorrect pilot-hole size, insufficient entry chamfer or inadequate chip-relief space can increase cutting load and reduce process stability.
Pilot Hole
Calculated for the ProfileThe pilot hole is selected according to the finished profile, material and machining conditions.
- Match the internal form geometry
- Consider the workpiece material
- Control straightness and position
- Avoid excessive remaining material
Entry Chamfer
Support Smooth EngagementThe chamfer provides clearance for the outside corners of the broach as cutting begins.
- Chamfer should reach the form corners
- Maintain a clean, concentric entrance
- Reduce impact during initial contact
- Match the broach and part geometry
Bottom Relief
Provide Space for ChipsInternal rotary broaching pushes displaced material and chips ahead of the cutting face.
- Allow clearance beyond the form depth
- Avoid chip packing in blind holes
- Consider through-hole conditions
- Use suitable cutting fluid
Common Rotary Broach Profiles
Standard and customized broaches can produce several internal drive forms and precision polygon features.
Hexagonal
Used for socket screws, fittings, precision fasteners and internal wrenching features.
Square
Suitable for square drives, adjustment features and specialized mechanical components.
Torx-Style
Six-lobe profiles should be specified by the required size, technical drawing or applicable standard.
Special Profiles
Splines, serrations and customized forms can be manufactured according to the customer’s drawing.
Information Required to Select a Rotary Broach
Complete application details help determine the broach geometry, holder compatibility and suitable machining setup.
Hexagonal, square, Torx-style, spline or another customized internal form.
Provide the across-flats size, major diameter, tolerances and corner requirements.
Confirm the finished depth and the available relief space behind the internal form.
Material grade, hardness and heat-treatment condition influence tool and parameter selection.
CNC lathe, Swiss-type machine, screw machine or machining center and available holder space.
Production volume and current machining conditions help determine the appropriate solution.
Rotary Broaches for Precision CNC Applications
PRONIXT supplies standard and customized rotary broaching tools according to the required form, dimensions, material and machine application.
Powder-metallurgy high-speed steel provides hardness, toughness and wear resistance.
TiCN coating is available for improved wear resistance in suitable applications.
Coating selection can be adjusted according to the material and machining conditions.
Special forms, dimensions and shank configurations can be manufactured from confirmed drawings.
Common Rotary Broaching Problems
If form accuracy or tool life is unstable, evaluate the complete setup rather than checking only the broach.
Rotary Broaching FAQ
Can rotary broaching produce a complete form in one pass?
Which machines can use rotary broaching tools?
Can stainless steel be rotary broached?
Is the pilot hole the same size as the finished form?
Can PRONIXT produce customized rotary broaches?
Need Help Selecting a Rotary Broach?
Send us the required form, dimensions, broaching depth, workpiece material, machine model and technical drawing for evaluation.
Comments
One response to “What Is Rotary Broaching? How Internal Hex, Square and Torx Forms Are Made”
[…] Read the Article Frequently Asked Questions […]